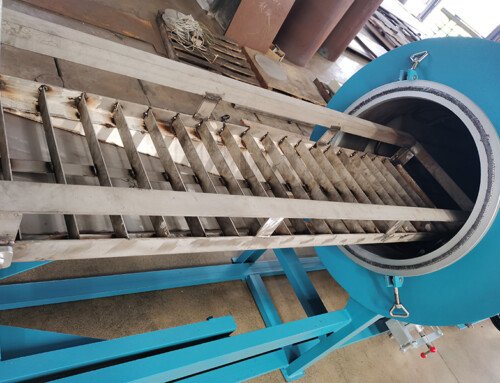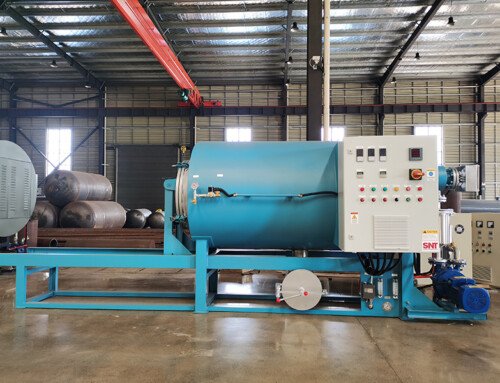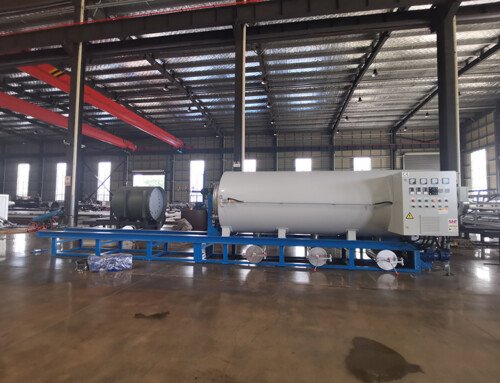
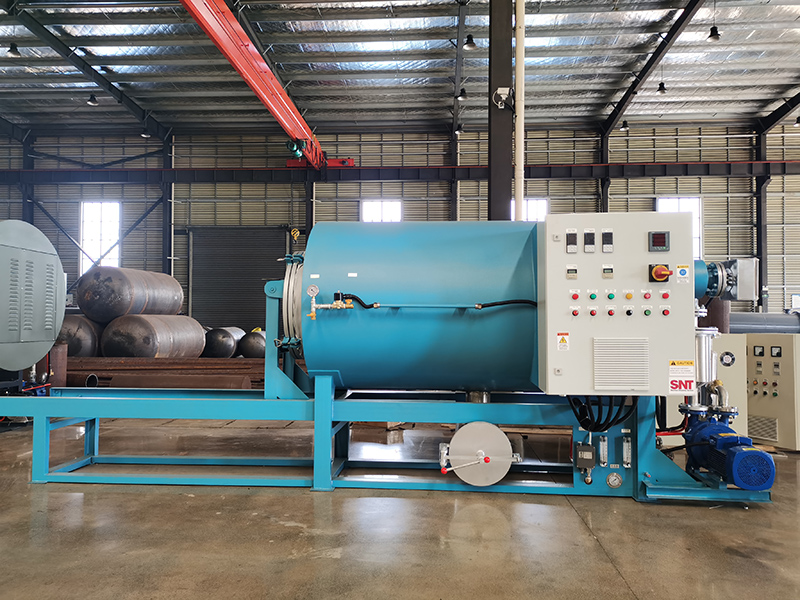
Screw cleaning furnace aging precursor judgment helps maintenance teams catch hidden performance degradation long before unplanned breakdowns interrupt scheduled production cycles. Many aging issues do not appear as sudden, obvious failures; they build slowly over hundreds of heating and cooling cycles, creating subtle, easy-to-miss warning signs that only become critical after the furnace has already been operating at reduced efficiency for weeks or months. A structured, regular assessment workflow identifies these early signals, so teams can schedule targeted maintenance during planned downtime instead of dealing with costly, unexpected stops in the middle of a production run.
Heating Element Performance Drift and Thermal Uniformity Shifts
Heating element performance drift and thermal uniformity shifts are one of the earliest and most reliable signs of furnace aging, as repeated cycles of extreme high heat and rapid cooling gradually degrade the heating system’s ability to maintain consistent, even temperatures across the entire working chamber. When heating elements begin to age, their resistance changes slowly over time, creating uneven heat distribution that cannot be fully compensated for by the control system’s default tuning parameters. This drift often goes unnoticed at first, because the control system will push the remaining healthy elements to work harder to try to hit the set temperature, masking the underlying degradation until multiple elements begin to fail.
The assessment process starts by running a full temperature mapping test across every defined measurement point inside the chamber, at multiple set temperature levels covering the full normal operating range. Teams compare the new temperature uniformity data against the original baseline readings taken when the furnace was first commissioned, to spot any new hot spots or cold zones that did not exist before. They also track total heating time required to reach the target operating temperature, and record how long the heating elements stay energized during a normal heat preservation cycle. A noticeable, consistent increase in total heating time, or a growing gap between the highest and lowest measured chamber temperature, is a clear early warning that the heating system is beginning to age and will need targeted attention soon.
Seal Degradation and Unintended Pressure Deviations
Seal degradation and unintended pressure deviations signal that the furnace’s closed chamber sealing system is losing its ability to maintain a stable, controlled internal environment. The high temperature, chemically aggressive fumes generated during the cleaning process slowly break down seal materials over repeated cycles, creating tiny, almost invisible leaks that alter the internal pressure balance. These leaks do not create obvious, visible smoke or pressure loss at first, but they gradually reduce process efficiency and create safety risks that grow worse with every additional operating cycle.
Teams can spot these early warning signs by monitoring the exact amount of time the furnace takes to pull down to its target operating vacuum level at the start of each cycle. A slow, steady increase in the time required to reach the set vacuum pressure, or a small but measurable rise in internal pressure that happens naturally during the heat preservation phase, indicates that the seals are no longer forming a perfect airtight barrier. Additional checks include running a static pressure hold test after the chamber is fully sealed, with no active vacuum or gas purge running, to measure how much pressure drifts over a fixed 30 minute period. Even a small, consistent upward drift in internal pressure during this test confirms that seal degradation has begun, long before the leak becomes large enough to cause a full process failure.
Control System Response Lag and Calibration Drift
Control system response lag and calibration drift reveal that the furnace’s core sensing and regulation components are aging and no longer reacting to changing conditions with the same speed and accuracy they did when new. After thousands of high temperature cycles, temperature sensors begin to develop calibration offset, pressure transducers lose measurement precision, and control loop processing logic develops small, unplanned delays that prevent the system from making fast, precise adjustments. These issues often show up as small, unexplained fluctuations in process readings that the control system cannot smooth out, even after a full standard recalibration.
The assessment process starts by comparing readings from the furnace’s built-in temperature and pressure sensors against external calibrated reference instruments that are traceable to metrology standards. Any consistent, repeatable offset between the furnace’s internal readings and the reference measurements that cannot be fixed with a simple routine recalibration confirms that the sensing components have begun to age. Teams also measure the total response time between the moment the system sends a command to adjust heating power or gas flow, and the moment the corresponding physical change registers on the reference measurement tools. A noticeable increase in this response lag, or small, unprompted fluctuations in control output that do not match real changes in chamber conditions, are clear signs that the control system’s core components are degrading.
Insulation Material Degradation and Unusual External Surface Temperature Rise
Insulation material degradation and unusual external surface temperature rise is a physical aging signal that is easy to overlook, but directly impacts both energy efficiency and overall equipment safety. Years of repeated exposure to extreme internal heat, combined with minor exposure to process fumes that seep through small seal gaps, gradually break down the thermal insulation material inside the furnace chamber walls. As the insulation loses its ability to trap heat inside, more and more thermal energy escapes through the outer furnace shell, raising the temperature of external surfaces far above their original normal operating levels.
Teams can check for this early precursor by using a non-contact temperature measurement tool to scan every external surface of the furnace during a full normal operating cycle, once the system has been running at its maximum operating temperature for several hours. They compare these readings against the original baseline external temperature map recorded when the furnace was new, to spot any sections of the outer shell that are now running noticeably hotter than they were originally. A clear, localized hot spot on the outer chamber wall, or a general rise in average external surface temperature across the whole furnace, confirms that the internal insulation has begun to break down. This issue not only wastes large amounts of energy, it also creates a risk of accidental contact burns for operators, and can raise the temperature of nearby electrical components to unsafe levels.
Exhaust System Backpressure Drift and Residue Buildup
Exhaust system backpressure drift and residue buildup shows that the fume extraction and exhaust path components are slowly becoming clogged with hardened process residue, after hundreds of cleaning cycles. Over time, the volatile material removed during the screw cleaning process condenses and solidifies inside exhaust pipes, filter assemblies, and exhaust treatment components, gradually reducing the total open cross section of the exhaust path. This creates a slow, steady rise in system backpressure that reduces the furnace’s ability to properly vent process fumes, even when no obvious blockage is visible.
Maintenance teams track exhaust system backpressure readings at a fixed point in the exhaust path, during the exhaust purge phase of every standard cleaning cycle. A consistent, gradual upward trend in measured backpressure, even after routine filter cleaning or replacement, confirms that hardened residue is building up deeper inside the exhaust system where standard maintenance cannot reach. Additional signs include faint, unusual odors escaping around the furnace chamber door during operation, or longer than normal exhaust clearing times at the end of each cleaning cycle. Catching this aging precursor early prevents complete exhaust blockages that can cause dangerous pressure buildup inside the chamber, or force the furnace to shut down mid-cycle to avoid unsafe operating conditions.