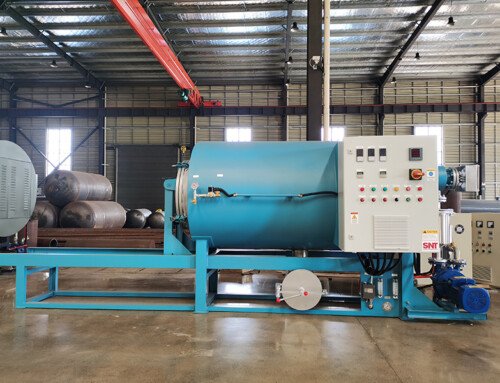
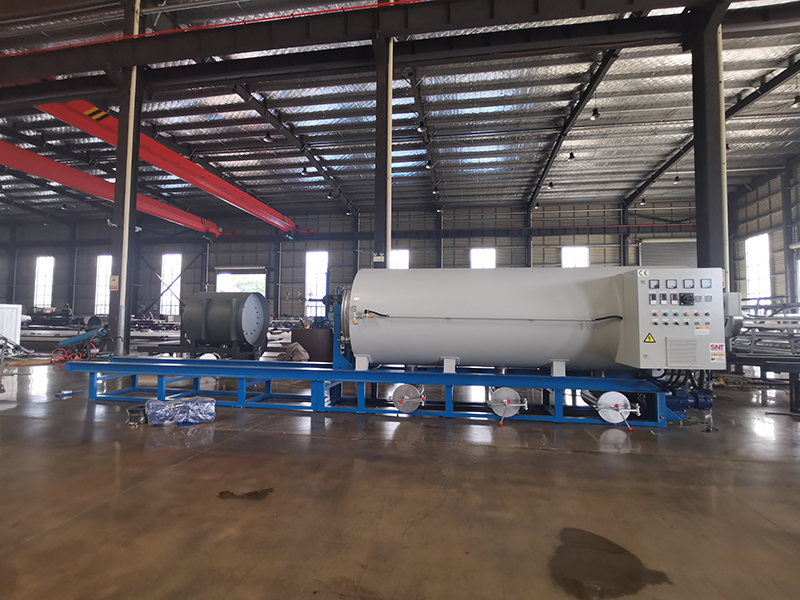
Batch type burn off oven systems are widely used across industrial finishing operations to strip accumulated paint, powder coating, and organic process residue from production racks, fixtures, and reusable metal parts that see repeated coating cycles. Unlike abrasive blasting or chemical stripping methods that can wear down base metal surfaces or generate large volumes of hazardous waste, this thermal process breaks down organic coating layers in a controlled high-temperature environment, leaving the underlying metal substrate intact and ready for re-use. When operated with consistent procedural discipline, this approach delivers uniform, thorough coating removal even for complex geometric parts with narrow gaps, threaded holes, and internal cavities that trap residual coating after repeated production runs.
Pre-batch part sorting and chamber loading preparation
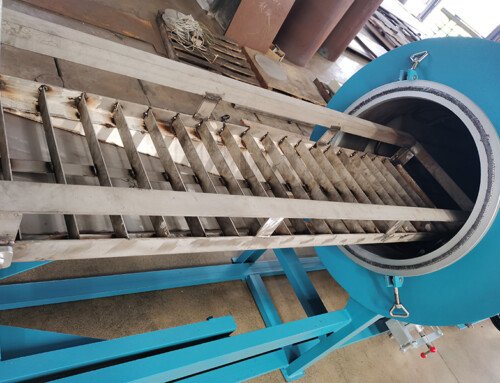
Before any parts are placed into the chamber, sort all incoming items to separate thin, high-tolerance metal fixtures from heavy, thick steel racks that can withstand extended high-temperature exposure, so you can group parts with similar thermal resistance together to create a balanced, predictable heating cycle. Scrape off any large, thick chunks of loosely adhered surface coating by hand before loading, to reduce the total volume of material that will decompose during the cycle and prevent unexpected spikes in fume output that can disrupt process stability. Arrange all parts on dedicated support racks with clear, open gaps between every component, so circulating hot air can reach every surface evenly without creating shadowed zones where trapped coating might not fully decompose. Document the total part count, primary coating type, and approximate total coating volume for every batch before starting the cycle, so you can reference this data later to refine process parameters for future similar cleaning jobs.
Controlled thermal cycle operation and process oversight
Initiate the cycle with a slow, gradual heat ramp that raises chamber temperature at a steady, pre-defined rate, to avoid rapid thermal expansion that could create warping, thread deformation, or micro-cracking in precision machined metal fixtures. Maintain a low-oxygen environment during the main decomposition phase, so coating layers break down through controlled pyrolysis rather than uncontrolled open flame combustion, preventing localized hot spots that could discolor or permanently damage the base metal. Monitor chamber temperature, airflow circulation, and exhaust emission conditions continuously for the full duration of the cycle, making small incremental adjustments as needed to keep all operating parameters within the validated safe range for the specific batch of parts being processed. Once the primary pyrolysis phase is complete, transition the system into a regulated secondary oxidation stage that breaks down any remaining thin, partially decomposed coating traces, ensuring no sticky, semi-burned residue is left clinging to part surfaces.
Post-cycle cooling, part retrieval and secondary cleanup
After the full thermal cycle concludes, run a slow, controlled cool down sequence that brings chamber temperature down gradually over an extended period, rather than venting in large volumes of cool ambient air to speed up the process. This gradual cooling phase prevents rapid temperature contraction that could create thermal stress or dimensional distortion in metal parts that hold tight tolerance requirements for subsequent production use. Once all parts have cooled completely to a safe handling temperature, remove them from the chamber and perform a quick visual check to confirm all coating layers have been fully decomposed, leaving only a thin, harmless layer of inorganic ash that wipes away easily with a dry cloth or low-pressure clean air blast. Log all key cycle parameters, final part condition observations, and any minor adjustments made during the process, to build a growing reference library that makes every subsequent coating removal run more consistent and reliable over long-term operation.